Start with the part, not the machine
Hold the part up and ask whether it is hollow. A bottle, jerrycan or tank is hollow, so it is blown. A cap, crate, housing or pail is solid-walled and molded in a closed cavity, so it is injected. Most PET beverage bottles use both machines in sequence, which is why plants often buy the two together.
| Process | Makes | Where it is strong | Watch out for |
|---|---|---|---|
| Stretch blow molding (PET) | Water, soda, dairy, oil bottles | High speed, light clear bottles, rotary layout | Needs preforms, plus a big air supply |
| Extrusion blow molding | Drums, jerrycans, tanks, odd shapes | Large volumes, handles, short mold lead time | Parison wall control, trim waste |
| Injection blow molding | Small bottles, pharma and cosmetic | Accurate neck, no trim | Higher mold cost, small volumes |
| Injection molding | Closures, crates, pails, technical parts | Detail, repeatability | Mold size and clamp force |
One maker’s published comparison puts extrusion-blown volumes from a few millilitres up to tanks of thousands of litres, and injection-blown bottles in the 5 to 300 ml range. Treat those as typical bands, not guarantees.
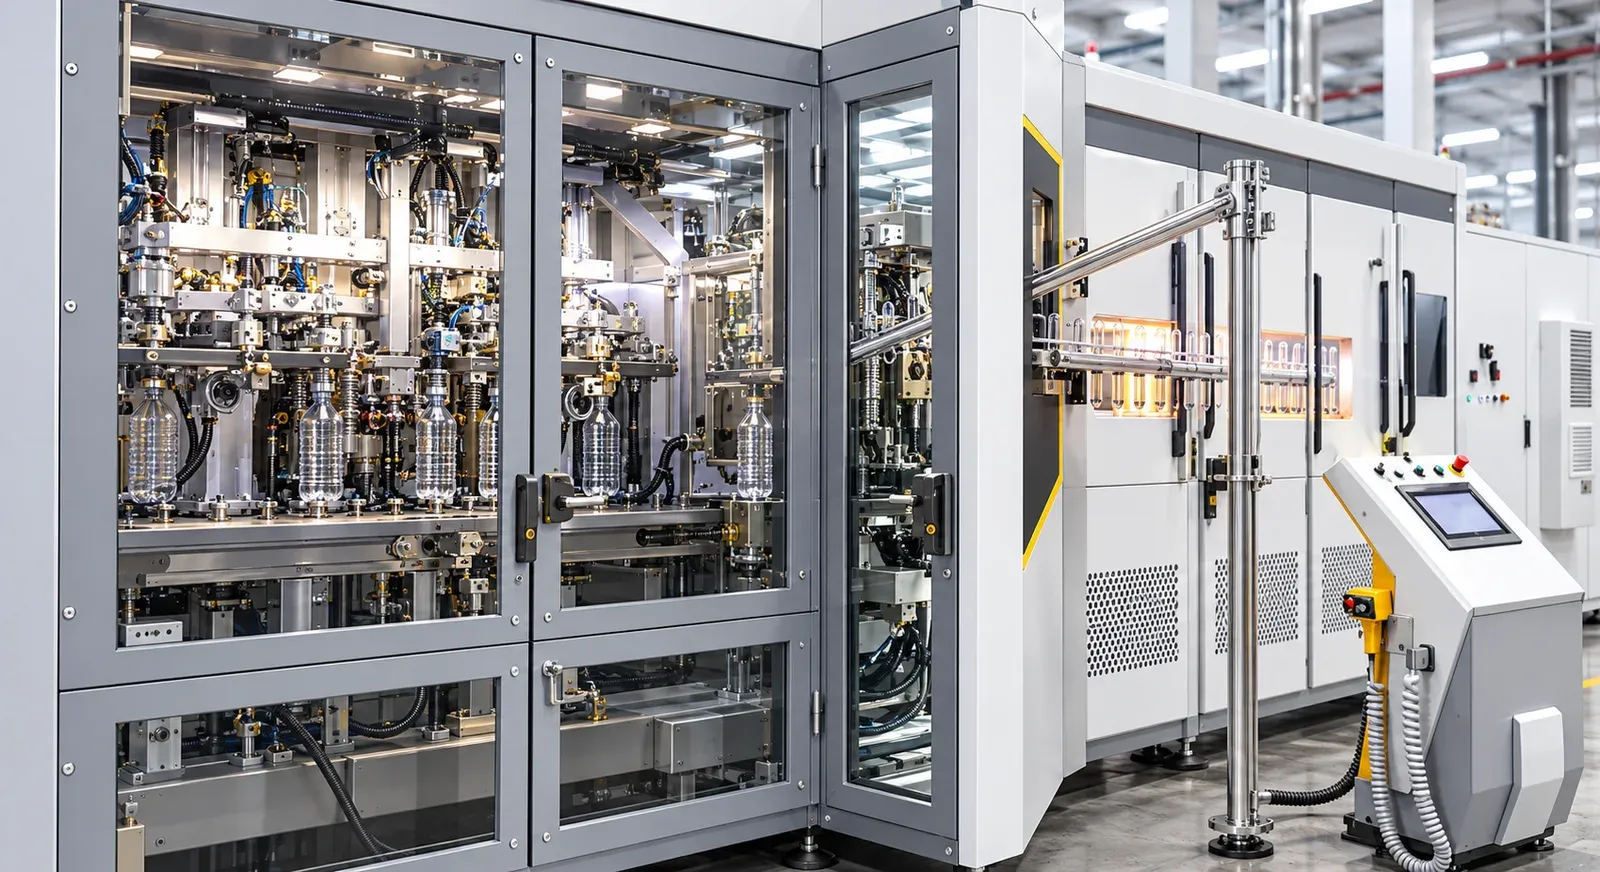
Our PET stretch blow molder
The automatic rotary machine heats preforms in an infrared oven at about 90 to 110 °C, then stretches and blows them on a wheel of mold sets. Our sub-series cover bottles from 0.25 to 20 L; no single model spans that whole range. Rotary machines commonly carry 6 to 24 cavities. As a planning example, 12 cavities on 500 ml water bottles at about 1,500 bottles per cavity-hour gives 18,000 bottles per hour. That is an illustration, not a quoted rating.
Budget the utilities as seriously as the machine: high-pressure air at about 3.0 to 4.0 MPa, low-pressure air at 0.6 to 1.0 MPa, and mold cooling water at about 8 to 12 °C. Read the Automatic Rotary PET Bottle Blow Molding Machine page for neck finishes (28 to 55 mm) and line linking to filling and capping.
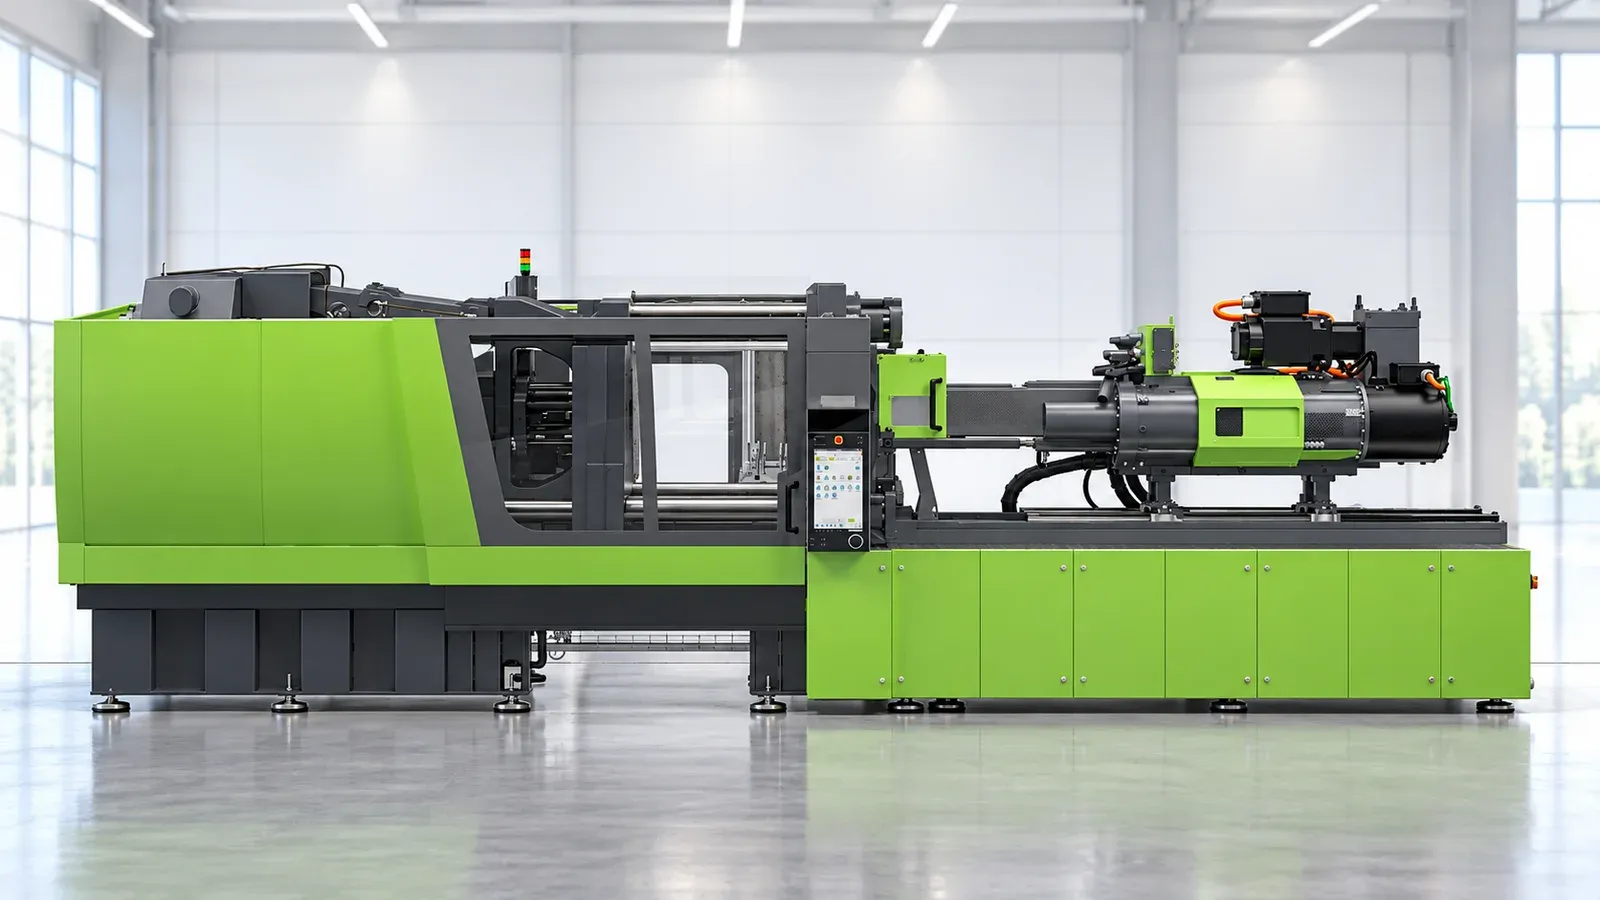
Our all-electric injection machine
The 5000 kN All-Electric Injection Molding Machine is a horizontal machine with servo drives. Typical data: tie-bar spacing about 800 to 1,050 mm, shot volume about 1,000 to 3,000 cm³ depending on the screw, opening stroke 900 to 1,200 mm, mold weight up to about 5 to 10 t, dry cycle 3 to 6 seconds, installed power 60 to 110 kW and machine weight 20 to 30 t. Check floor loading and crane capacity before you order. Clamp force must exceed the projected area times cavity pressure, and the full method is in our clamping force guide.
Power and plant checks
Confirm your supply (for example 380 V at 50 Hz or 440 to 480 V at 60 Hz) and compressed air capacity before comparing machines. Hot climates raise chilled-water load for both processes.
What to send for a quote
- Bottle or part drawing, or a physical sample, with weight
- Material grade and, for PET, the preform neck finish and weight
- Hourly output or annual volume, and cavities if you know them
- Filled product: water, carbonated, hot-fill, dairy or oil
- Auxiliaries wanted: robot, dryer, chiller, compressor, conveyor
- Local voltage, frequency and available floor area
Other process lines are listed on the Industrial Manufacturing page.